
Dehumidifiers
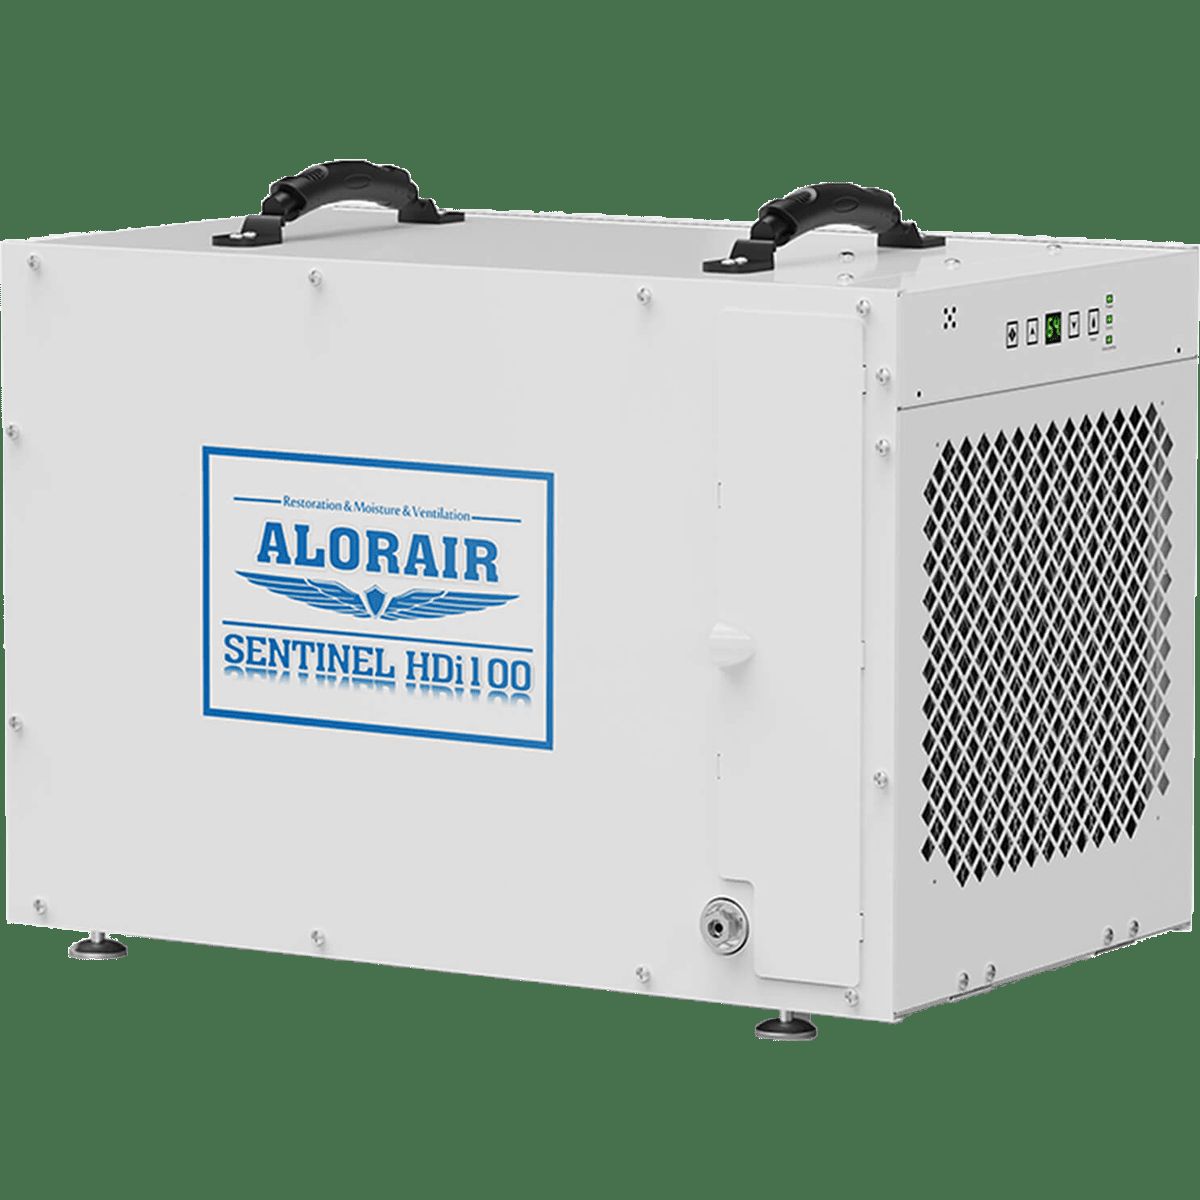
For dehumidifying areas up to 2,900 square feet, the AlorAir Sentinel HDi100 will get the job done without requiring a lot of monitoring or oversight. Equipped with a heavy-duty internal condensate pump, this durable machine removes up to 100 pints of moisture per day at AHAM. Set the HDi100 up in your crawl space or basement; use it in remote storage units, warehouses, businesses, and more for reliable humidity control and moisture removal. Defeat Damaging Moisture To win the battle with high humidity and unwanted moisture, you need a reliable machine that can be monitored and controlled remotely when needed. The Sentinel HDi100 has the features that equip it to do all this and more. High Performance Capacity at AHAM (80° F—60% RH) = 100 pints/day (15.7 gallons) Capacity at Saturation (90° F—90% RH) = 220 pints/day Capacity at DOE (73° F—60% RH = 78 pints/day) Low Temperature Operation/Wide RH Range Temperature Range: 33.8° F—104° F Relative Humidity Range: 36%–90% RH Internal Condensate Pump – Includes Drain Line (19.6 ft.) Pump accumulated condensate vertically or horizontally up to 14.7 feet. Set up for gravity draining and use the pump only when needed. Designed to Endure The AlorAir Sentinel HDi100 is designed with internal parts that help it operate efficiently and effectively over a longer period of time. Rare Earth Alloy Tube Evaporator: This innovative feature extends the life of the coils by providing protection against leakage and maintaining the coil’s heat transferability. Microchannel Condenser Technology: Improves the 50% dispersion effect of the condenser, 30% heat exchange area, and 50% refrigerant quantity for increased efficiency. MERV-10 Filter & Pre-Filter: By using a higher-level MERV-10 filter along with a clean air pre-filter, the internal parts are better protected against intrusive dust. In addition to these, the rotary compressor and by-pass air sensor enable the dehumidifier to operate even more efficiently. Additional Features Built